CAT 120M / 12M Motor Grader Parts — Circle Drive, Blade and Cylinder Wear List for African Haul Roads
Haul roads are the hardest grader duty there is
A grader maintaining a mine haul road works under continuous blade load, in abrasive material, for ten hours or more per shift. Every component between the circle and the cutting edge is under sustained stress, and the dust load accelerates wear on anything that moves against a wear surface.
The consequence is a very consistent failure order: circle drive first, then wear strips, then cylinders, then cutting edges. Fleets that plan against that order spend less and stop less than fleets that replace on failure.
| System | Typical symptom | First field check | Usual fix |
|---|---|---|---|
| Circle drive | Circle slips, rotation notchy, noise | Measure spline and gear backlash | Spline shaft or gear set |
| Circle wear strips | Blade chatter, excessive clearance | Measure strip thickness and clearance | Wear strip set |
| Blade lift cylinders | Blade drifts, slow lift | Check external leak and drift rate | Seal kit or cylinder |
| Cutting edges and end bits | Poor cut, adapter damage | Measure remaining edge length | Edge and end bit set |
| Fuel system (C6.6 / C7) | Hard start, derating, smoke | Compare rail pressure with setpoint | Injector plus code entry |
Circle drive: the spline shaft and the wear strips
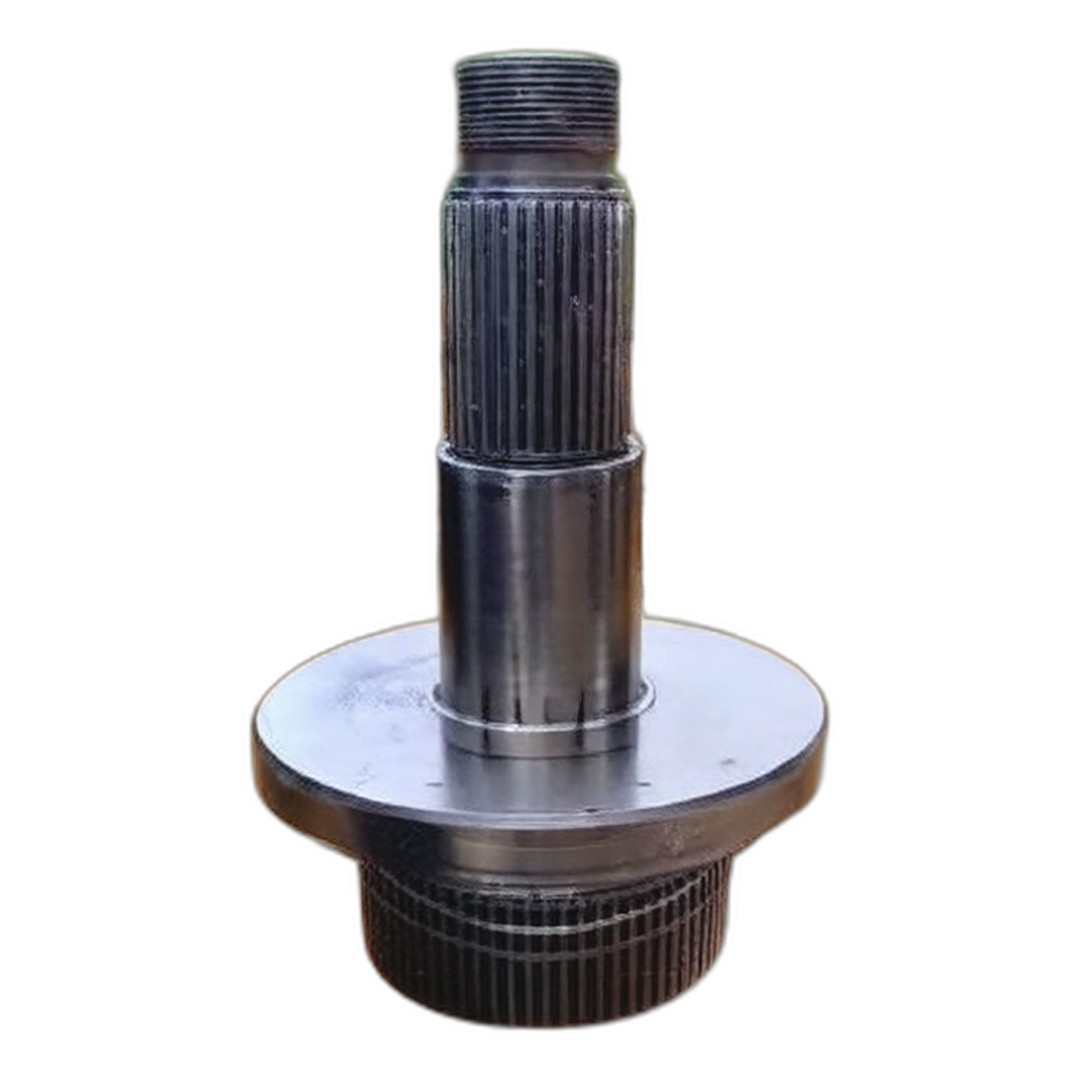
The circle drive is what lets the operator rotate the blade under load. When the spline shaft or the drive gear wears, the circle slips and the operator loses the ability to hold a precise angle — the machine becomes slow and the road surface suffers long before anything actually breaks.
We supply 307-1958 circle drive spline gear for the 120M and 140M range. Backlash measurement is the trigger: once it exceeds specification, replacing the spline before the gear is damaged is far cheaper than replacing both.
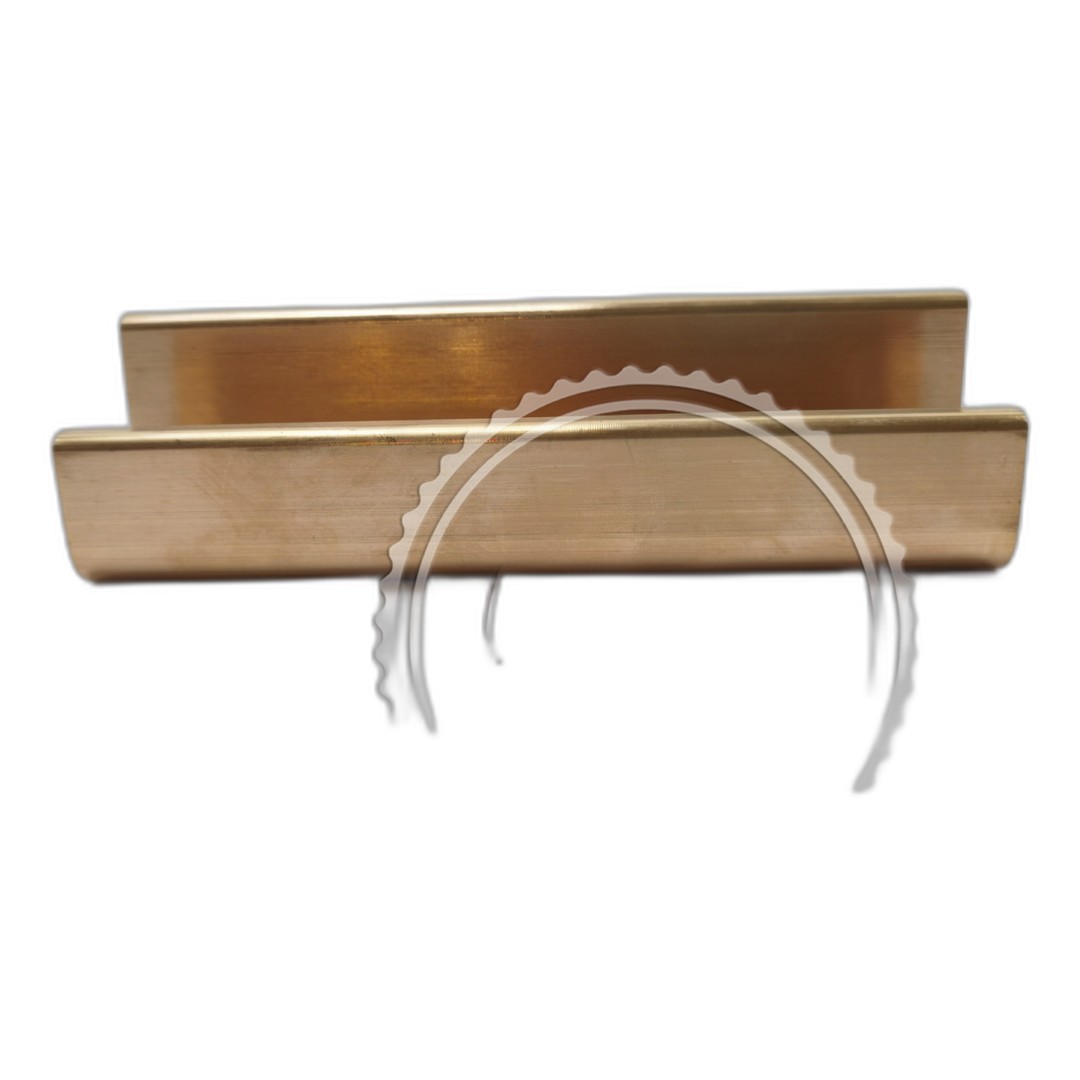
The companion item is 446-1526 wear strip. Wear strips are cheap and they are what keeps the circle running true; running them to metal-on-metal is what destroys the circle itself.
Blade lift and articulation cylinders
Blade drift is normally a seal problem, not a cylinder problem. Measure the drift rate over a fixed period with the engine at operating temperature; if the cylinder rod has no scoring and the barrel is sound, a seal kit resolves it. Only external scoring or a bent rod justifies a complete cylinder.
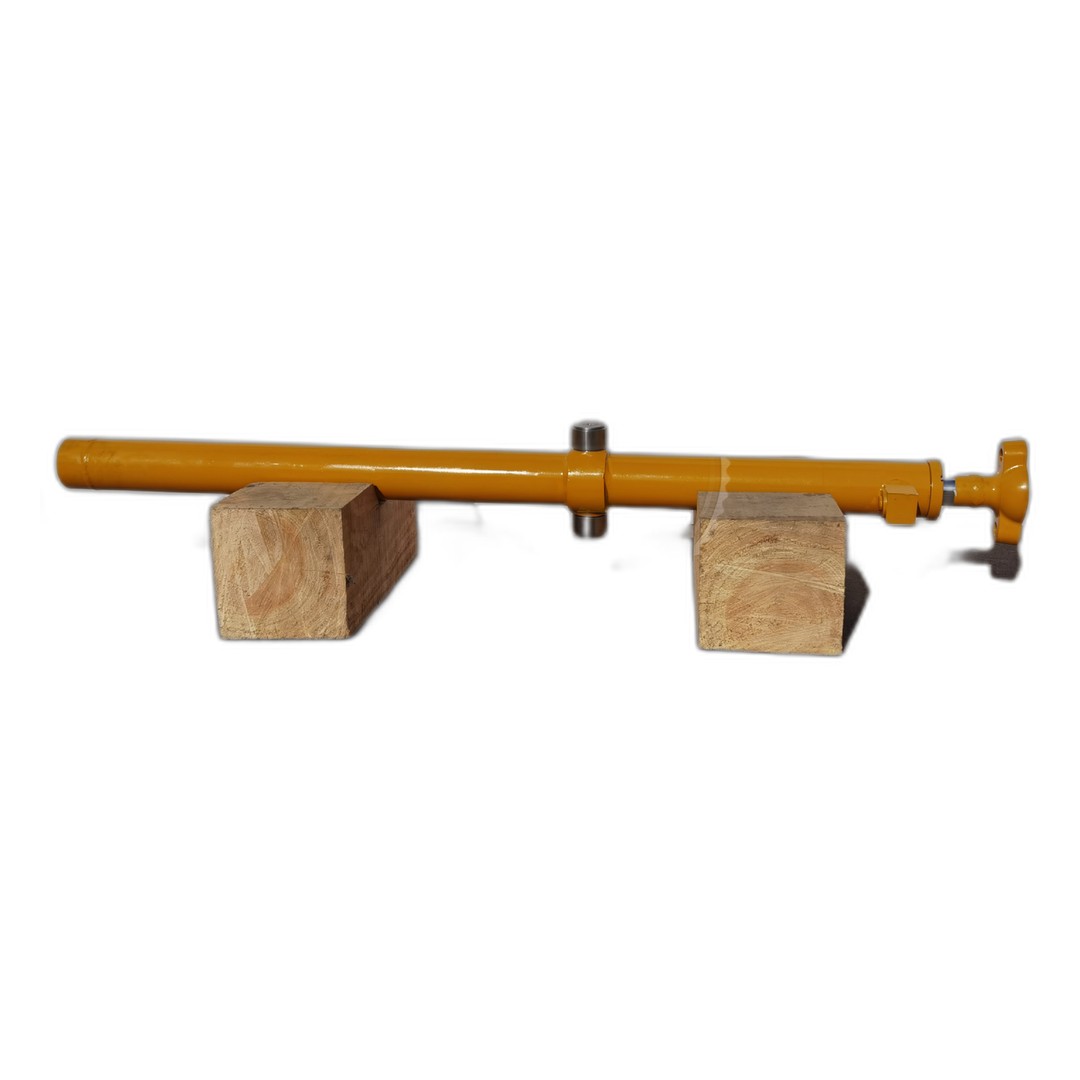
On the 12M we supply 270-7534 blade lift cylinder, with 335-1974 for the 12M2 lift cylinder and 247-0096 for the articulation cylinder. All three are serial-number sensitive, so the PIN and the old part number are required before we ship.
Cutting edges, end bits and bushing sets
Cutting edges are consumables on a haul road grader, and the rule is simple: replace the edge before it wears back into the adapter. An edge is a fraction of the cost of an adapter set, and worn edges that reach the adapter also distort the moldboard.
We supply 7D-1577 cutting edge for the 140K, 120M and 12M range, and the 467-5183 bushing for the 120M and 140M linkage. Bushings should always be replaced with the pins as a set — a new bushing in an elongated bore fails quickly.
Fuel system on the C6.6 and C7 platforms
The 120M and 12M run on the C6.6 and C7 engine platforms with common rail fuel systems. Hard starting and derating on these engines is far more often an injector problem than a pump problem, and the check is straightforward: compare actual rail pressure with the setpoint before replacing anything.
The injector we supply most on this platform is 320-0690 for C6.6 applications. Injectors carry a trim code that must be entered into the ECM after installation; skipping that step leaves the engine running with unbalanced cylinders.
Packing and shipping to African mines
Stock items ship the same day. International express reaches most African mining destinations in 7 to 12 working days; cylinders, circles and heavy assemblies travel by sea, consolidated or full container, with transit confirmed against the destination port.
Everything is packed in wooden cases or heat-treated pallets, strapped, and documented with a packing list and loading photos before dispatch. To quote we need the machine PIN, the old part number and the mounting position.
Frequently asked questions
How do I know when the circle drive needs replacing?
Measure backlash. Once spline and gear backlash exceeds specification the circle will slip under load and the operator loses the ability to hold blade angle. Replacing the spline shaft at that stage avoids damaging the gear as well.
The blade drifts down. Do I need a new cylinder?
Usually not. Measure the drift rate with the engine warm; if the rod has no scoring and the barrel is sound, a seal kit resolves it. Only external scoring or a bent rod justifies a complete cylinder.
Can I replace just the bushings on the linkage?
Not usefully. A new bushing in an elongated bore fails quickly. Replace pins and bushings as a set, which is why we list 467-5183 alongside the matching pin.
How long does delivery to African mines take?
Stock items ship the same day and arrive in 7 to 12 working days by international express. Cylinders, circles and heavy assemblies go by sea, consolidated or full container, with transit confirmed against the destination port.
Need 120M / 12M grader parts pricing?
Send the machine PIN and the old part number — we confirm fitment and stock the same day.
WhatsApp +86 139 2519 9399 · Scan to send your part number, oropen the chat directly