CAT 993K Wheel Loader Parts: Oil Cooler, Hydraulic Cylinder and Check Valve Wear List for South American Copper Mines
Why altitude and ore dust hit 993K cooling first
At Andean mine altitude the air is thin, so radiator efficiency falls while the loader still runs full hydraulic load for two shifts. Fine copper ore dust coats the core and enters breathers, so oil temperature climbs and the hydraulic circuit starts to foam. The first symptoms are hot oil alarms, slow lift and tilt, and dark or milky oil - long before any mechanical breakage.
The chain runs like this: dust on core plus thin air - high oil temperature - oil thinning and oxidation - seal hardening - cylinder drift - check valve chatter - pump cavitation - rising back pressure on the engine. Blow the core from the clean side each shift, log oil temperature at full load and check the breather; all three checks are free and catch the chain early.
| Area | Symptom on site | Free first check | Usual fix |
|---|---|---|---|
| Radiator oil cooler | Hot oil, slow lift, foaming | Blow core from clean side, check breather | Clean or replace cooler |
| Hydraulic cylinder | Drift, weeping rod | Wipe rod, check for scoring | New seal kit or cylinder |
| Check valve | Chatter, pressure loss | Measure cracking pressure, inspect seat | New valve, flush line |
| Muffler | Loud exhaust, derate | Check for cracks and back pressure | New muffler, new gaskets |
| Hydraulic oil filter | Dark oil, slow response | Cut filter open, check water | New filter and oil |
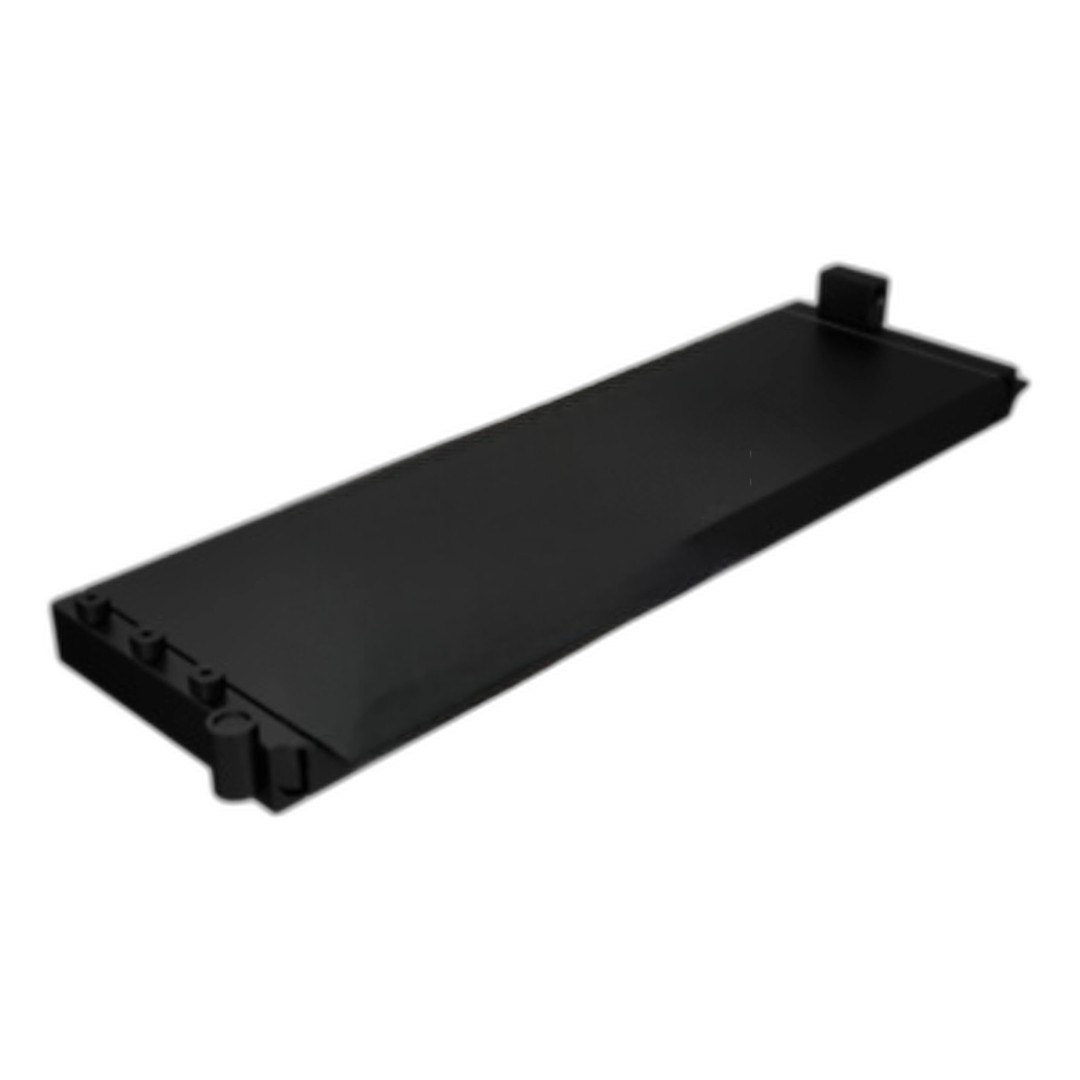
Radiator oil cooler 250-8480 CAT 993K Radiator Oil Cooler 250-8480 2508480 for Wheel Loader: clean before replacing at altitude
A hot oil alarm at altitude is not proof of a failed core. Blow the core from the clean side with low pressure air, verify fan drive and check the breather for dust cake. Many coolers recover completely after a proper clean. Only a recurring temperature rise with a clean core and correct fan speed justifies replacement.
Cooler 250-8480 CAT 993K Radiator Oil Cooler 250-8480 2508480 for Wheel Loader must be matched to core dimensions, port thread and mounting brackets; 993K and neighbouring loader models use different cores. On fitment, flush the oil lines, fit new filters and verify oil temperature at full load. Skip the flush and residual debris blocks the new core quickly.
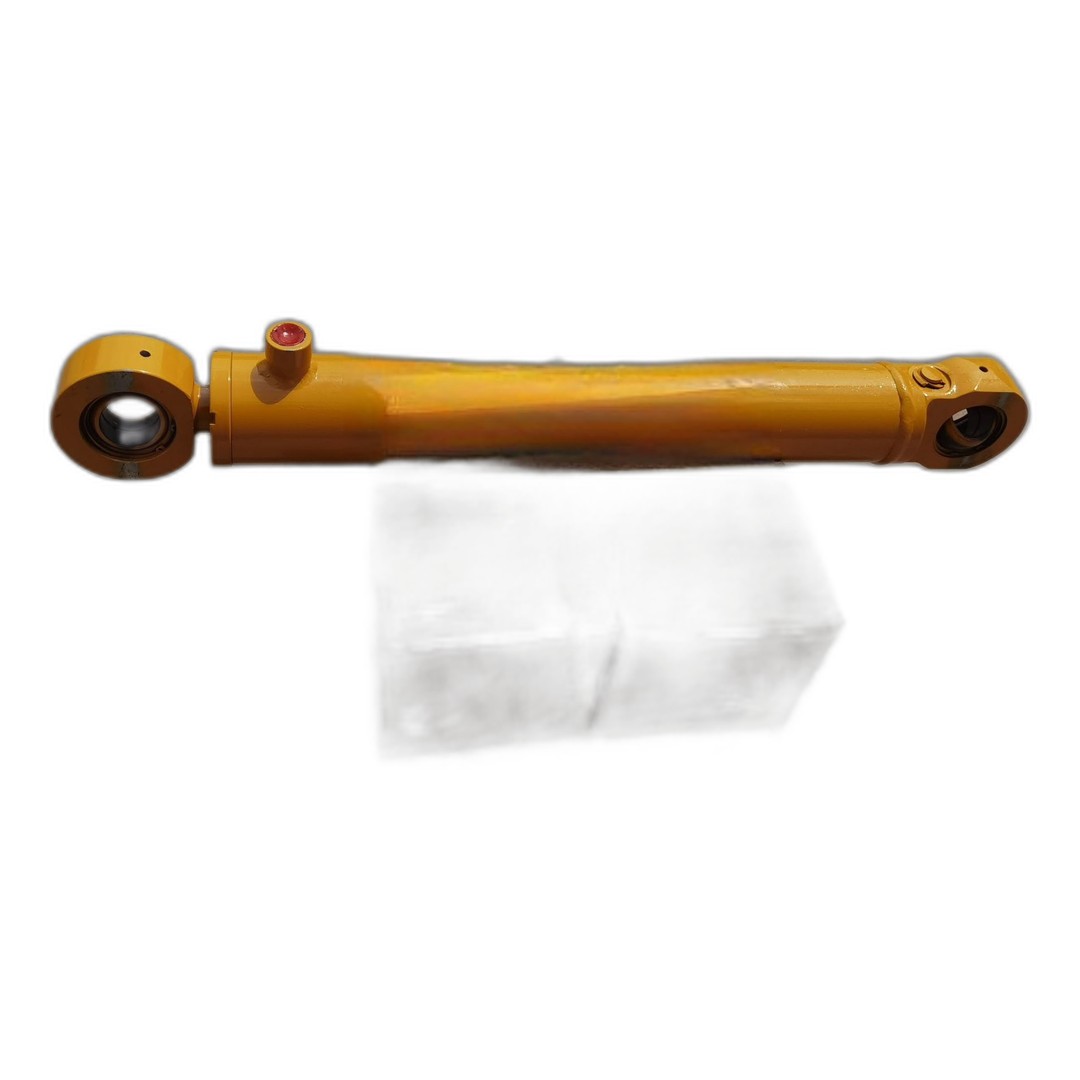
Hydraulic cylinder 288-5504 CAT 993K Hydraulic Cylinder and check valve 8E-6398 CAT 980G 992K 993K Check Valve 8E-6398 for Wheel Loader
Lift or tilt drift is usually a seal or valve problem, not a weak pump. Wipe the rod, inspect for scoring and measure cylinder drift over ten minutes with the engine off. A scored rod destroys a new seal kit within weeks, so fix the rod first. Cylinder 288-5504 CAT 993K Hydraulic Cylinder is listed for the 993K with several sibling references - confirm rod diameter, pin size and port thread before ordering.
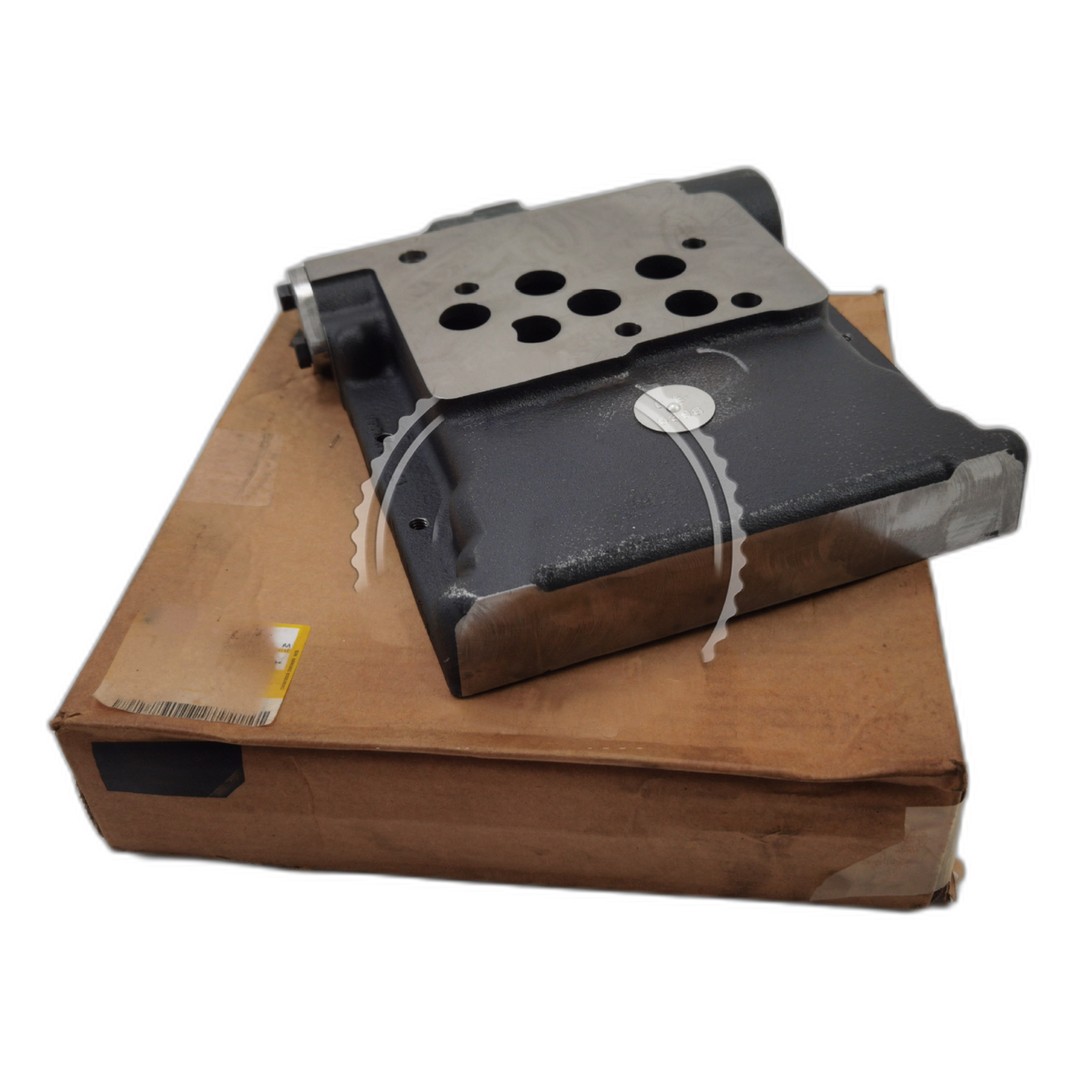
Chatter and pressure loss point to the check valve. Measure cracking pressure and inspect the seat for grit. Valve 8E-6398 CAT 980G 992K 993K Check Valve 8E-6398 for Wheel Loader is shared with 980G and 992K loaders, so confirm the set pressure, not just the shape. After fitting, flush the line and cycle lift and tilt ten times unloaded.
Muffler 312-5901 CAT 993K Muffler 312-5901 312-5900 358-0504 for Wheel Loader Engine and hydraulic oil filter 1328876 Excavator Parts Hydraulic Oil Filter 132-8876 1328876 Suitable for CAT 990H 992C 992D 992G
A cracked muffler raises back pressure, which at altitude shows up as derate, higher exhaust temperature and rising fuel use. Inspect weld seams and mounts, then measure back pressure before blaming the turbo. Muffler 312-5901 CAT 993K Muffler 312-5901 312-5900 358-0504 for Wheel Loader Engine replacement must include new gaskets and a mount check; vibration on ROM pads cracks rigid mounts quickly.
Filter 1328876 Excavator Parts Hydraulic Oil Filter 132-8876 1328876 Suitable for CAT 990H 992C 992D 992G is listed across several large CAT loaders, so match the thread, micron rating and bypass setting. Cut the old filter open at every 500 hour service - metal or grit there predicts cooler, cylinder and valve work weeks ahead. Cheap insurance on a two-shift mining loader.
Three rules for South American 993K copper fleets
1) Blow cooler cores from the clean side each shift and log full load oil temperature. Altitude plus ore dust is the number one avoidable cost. 2) Cut hydraulic filters open every 500 hours. Debris predicts cylinder and valve failure early. 3) Photograph every old part plate. Shared references across 980G, 992K and 993K are the top source of wrong shipments.
Follow these three and 993K hydraulic and cooling availability improves sharply. A copper mine measures tonnes loaded per shift, not the price of a single cooler.
Common spares and lead time reference
| Area | Typical part number | Suggested stock | Lead time from China |
|---|---|---|---|
| Radiator oil cooler | 250-8480 | 1 per 8 machines | 20 to 35 days |
| Hydraulic cylinder | 288-5504 | 1 per 10 machines | 20 to 35 days |
| Check valve | 8E-6398 | 1 per 6 machines | 10 to 18 days |
| Muffler | 312-5901 | 1 per 10 machines | 15 to 25 days |
| Hydraulic oil filter | 1328876 | 2 per machine | 8 to 15 days |
To San Antonio, Callao and mountain mine sites: filters, valves and sensors go by air; coolers, cylinders and mufflers are cheaper by sea. Mountain haulage and port congestion add two to three weeks, so order downtime parts at least six weeks ahead.
Frequently asked questions (993K South American copper mines)
Does a hot oil alarm at altitude mean the cooler is finished?
Usually no. Blow the core from the clean side, verify fan drive and check the breather for dust cake. Only a recurring rise with a clean core justifies replacement.
Will a 993K check valve fit a 992K or 980G directly?
Not always. The same reference is listed across the three loaders but set pressure and port thread can differ. Confirm the set pressure and send the serial number.
Is lift drift always a worn hydraulic pump?
No. Wipe the rod, inspect for scoring and measure drift over ten minutes with the engine off. A scored rod or a leaking check valve causes most drift.
Why does a cracked muffler cause a derate at altitude?
A cracked seam raises back pressure, which at altitude shows up as derate and higher exhaust temperature. Inspect welds and mounts, measure back pressure and fit new gaskets.
Need 993K pricing and lead time for a South American copper mine?
Send the machine serial number and the part numbers you need. We reply within 24 hours with price, stock and air or sea timing to San Antonio or Callao plus mountain haulage.
WhatsApp +86 139 2519 9399 · Scan to add WhatsApp and send part numbers Send message